Multistage centrifugal gas compressors
Designed and manufactured as per API 617.
The following drives are used:
– Synchronous or asynchronous electric motors (equipped with a frequency controller (VFD);
– Steam turbines made in compliance with API 611.
Centrifugal compressors are designed for the following process parameters:
– Capacity corresponds to inlet conditions: 500 to 150 000 m3/h;
– Discharge pressure up to 200 bar;
– Discharge temperature up to +200 °С.
Compressor inlet temperature varies over a wide range from -195 °С to + 100 °С.
The compressors are used to compress almost all types of gases, but most widely they are implemented for compression of hydrocarbons (HC), nitrogen (N2), natural gas (NG), including those with a high content of hydrogen sulfide (H2S). In this case, materials for the design of the compressor flow passage are selected in accordance with NACE MR 0175 / ISO 15156-1: 2001 (E).
Compressor units are completed with:
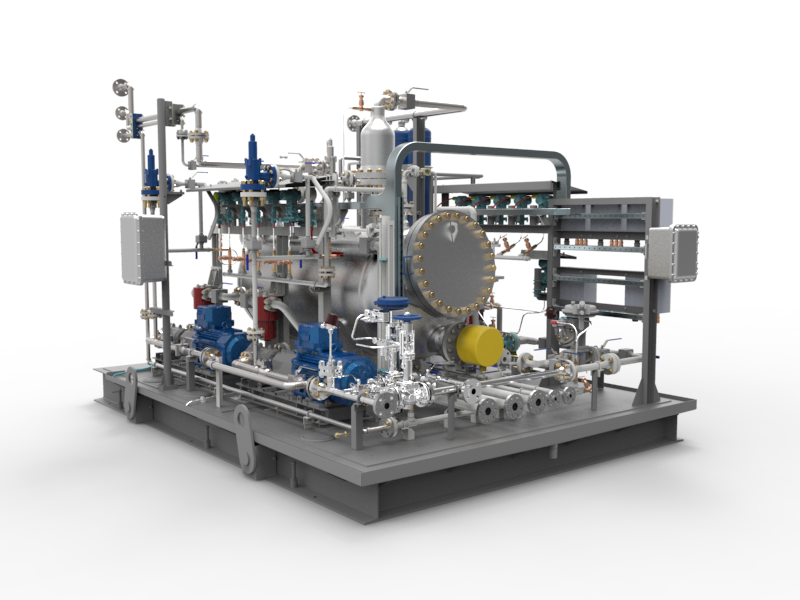
- Oil supply system made as per API 614 standard;
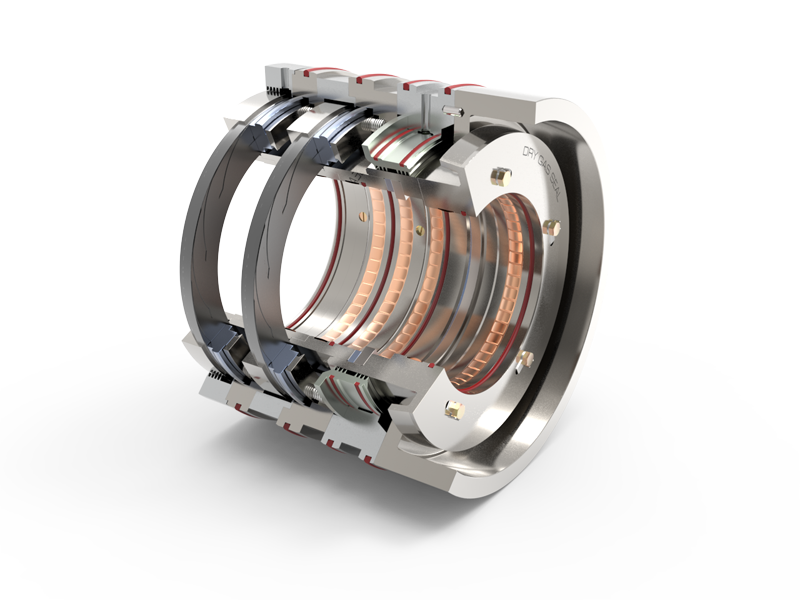
- Dry gas seal system as per API 692;
- Vibration monitoring system of the unit, in compliance with API 670;
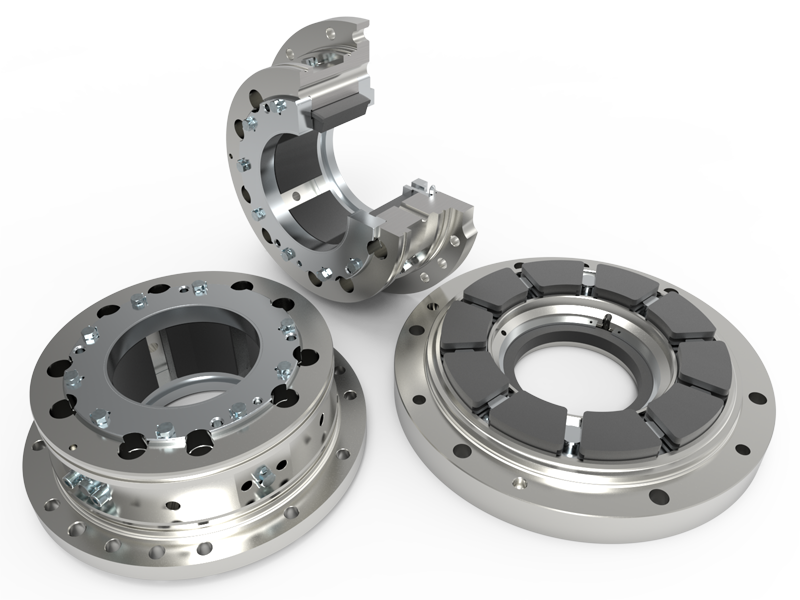
- Tilting pad type plain bearings;
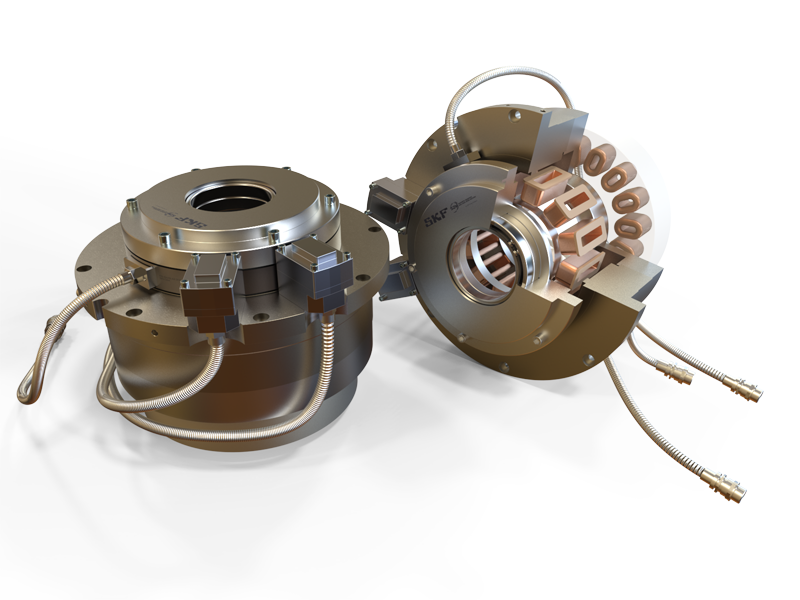
- Magnetic bearings;
- Anti-surge control system including anti-surge valve;
- Automatic control system (ACS);
If necessary, the compressor can be equipped with a multiplier conforming to API 613.
Compressor units are tested at the company’s benches and undergo a full range of inspections and checks in accordance with ITP, based on API 617 (chapter I & II) requirements they and include the following types of tests:
- HYDROSTATIC & GAS LEAKAGE TEST;
- IMPELLER OVERSPEED TEST;
- ROTOR BALANCING;
- MECHANICAL RUN TEST;
- PERFORMANCE TEST as per ASME PTC-10;
- COMPLETE UNIT TEST;
and others.
Applications of centrifugal compressors:
- Oil refineries;
- Chemical & petrochemical plants;
- Ethylene plants;
- Gas lift & gas injection applications, gas gathering;
- Transportation and storage of natural gas, including associated petroleum gas (APG).